State-of-the-Art Processing & Export Infrastructure
From temperature-controlled cold storage to automated sortex cleaning and insulated air freight packaging, our advanced facilities ensure zero quality loss from origin to destination.
State-of-the-Art Machine Lines & Infrastructure
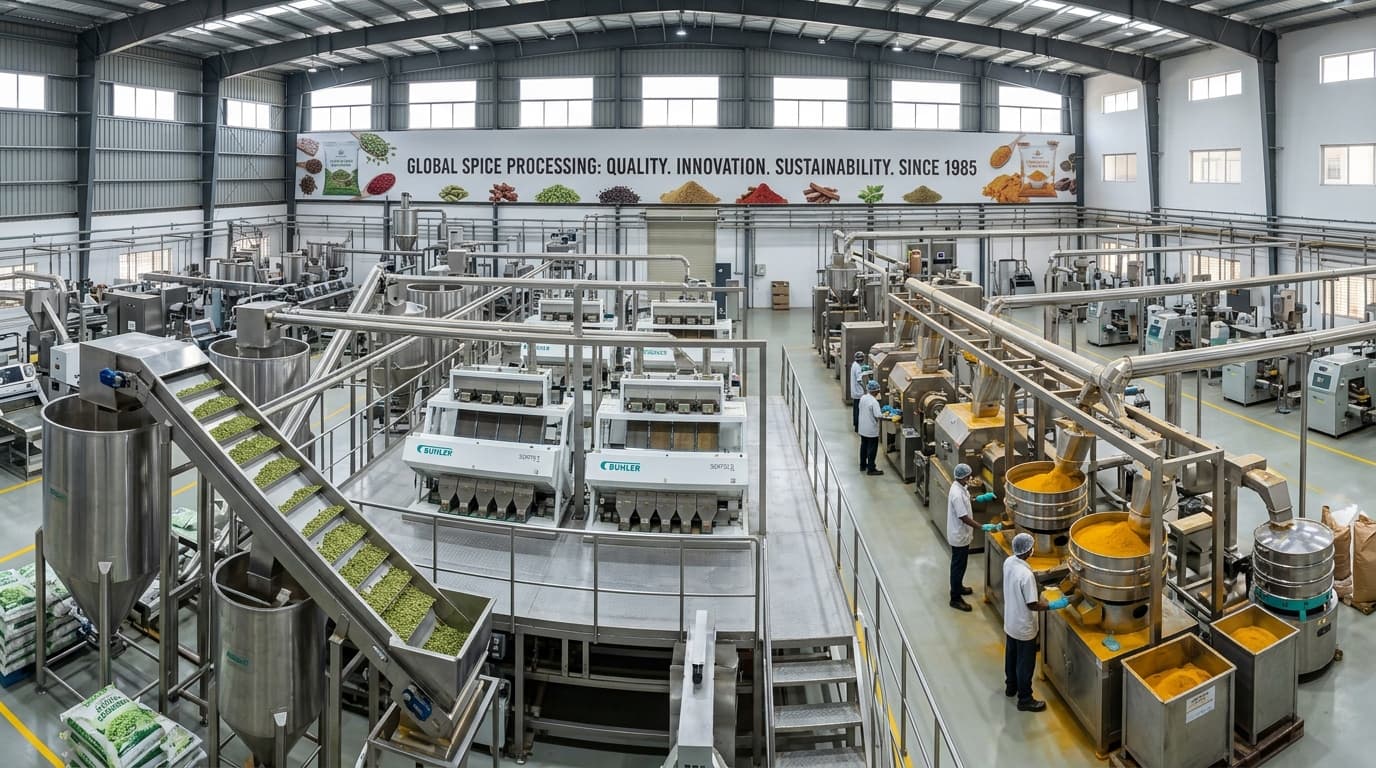
Our 60,000+ sq. ft. manufacturing facility is powered by a proficient R&D team and quality-driven machinery. Prior to processing, we wash seeds with pure water and utilize winnowing baskets for dusting before automated MTRA cleaning, gravity destoning, optical Sortex separation, and climate-controlled storage.
Pre-Cleaning & Seed Washing
Pure water seed washing, mechanical winnowing baskets, and dust extraction eliminate field dirt, stems, and initial impurities prior to high-tech processing.
MTRA Cleaner & Destoner
High-capacity MTRA seed separators and precision gravity destoners efficiently isolate stones, glass, heavy clods, and light foreign seeds.
Gravity Separator & Buhler Sortex
Advanced multi-channel optical Sortex cameras inspect color, size, and discolored seeds to achieve 99.9% purity and precise export grading.
Cryogenic Grinding & Metal Traps
Temperature-regulated pin mills preserve volatile spice aromas while powerful inline rare-earth magnet traps eliminate micro-metallic particles.
Cold Storage & Moisture Control
Humidity-controlled cold warehousing maintains optimal moisture (≤ 10-12%), preventing oil degradation and pest infestation without chemical additives.
Clean Room & Insulated Packing
Hygienic enclosed clean-room packaging utilizing airtight vacuum foil pouches, thermocol lining, and multi-ply food-grade bags.
In-House QC & R&D Laboratory
Fully equipped laboratory staffed by R&D specialists verifying curcumin percentage, volatile oil potency, moisture levels, and microbiological purity.
Factory Container Stuffing & Freight
Fumigated container stuffing directly at our plant premises with moisture absorbers for swift dispatch to airport and seaport cargo terminals.
State-of-the-Art Processing & Extraction Facility
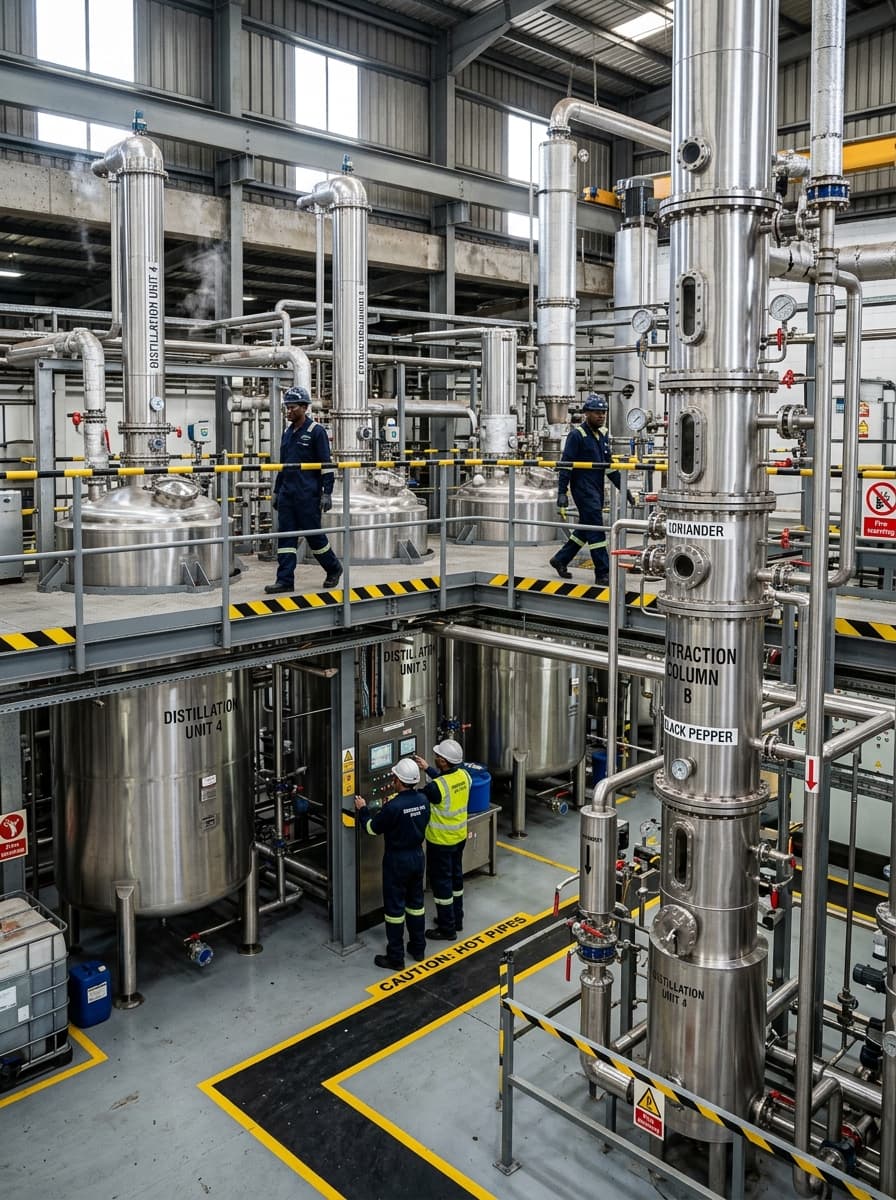
Our fully automated, state-of-the-art facility is equipped with advanced machinery designed for the efficient extraction of high-quality spice oils, optical color sorting, and cryogenic milling. The factory integrates precision controls and hygienic clean rooms to ensure consistency, purity, and compliance with global standards.
In-House QC Testing Laboratory
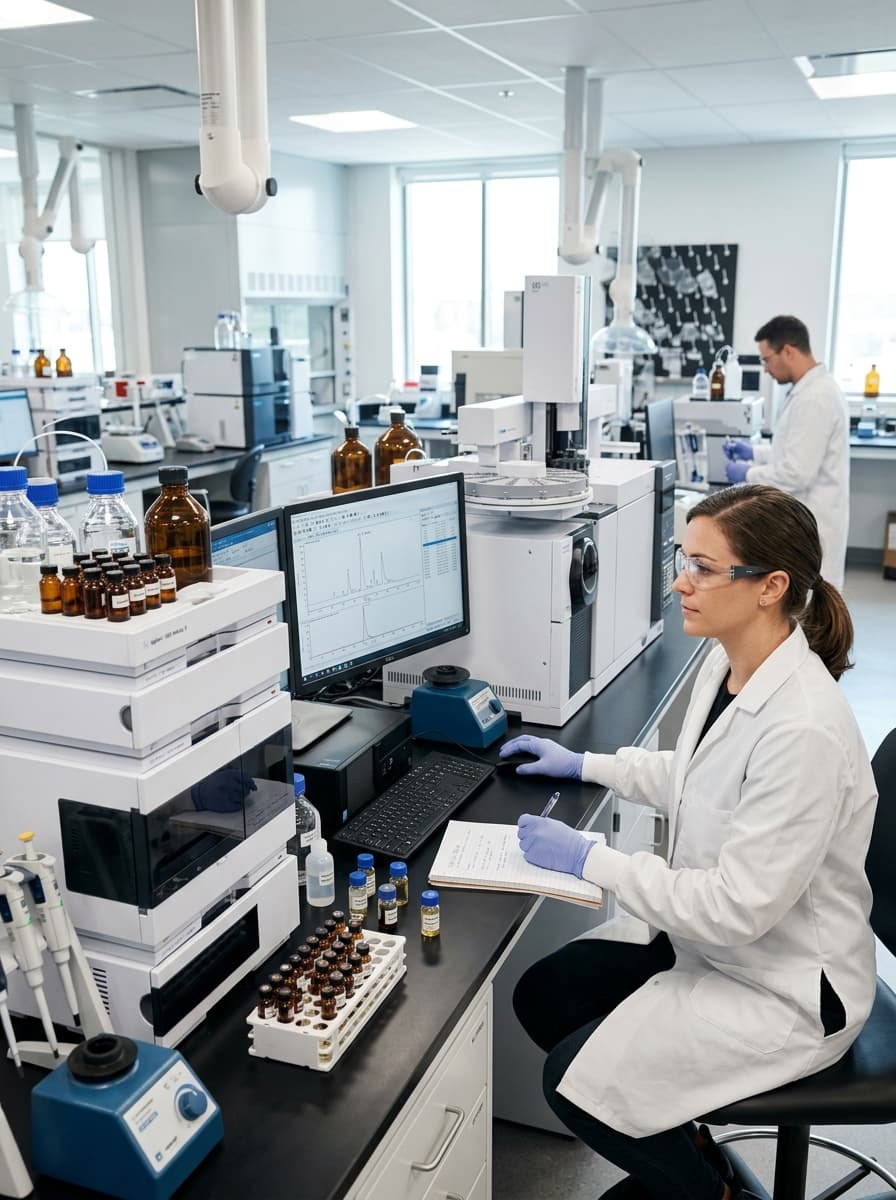
Equipped with advanced gas chromatography and spectrophotometers to analyze volatile oil levels, moisture content, and curcumin purity.
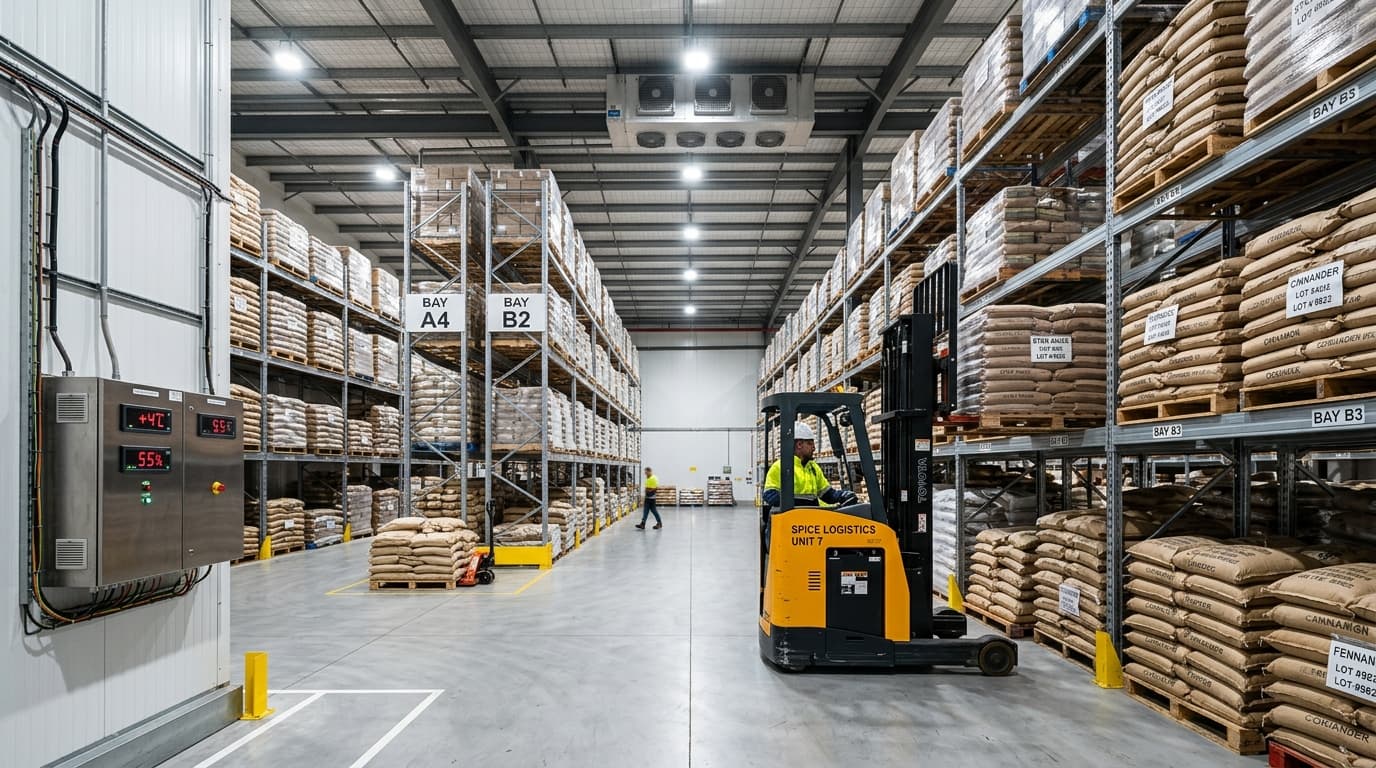
Climate Cold Storage Facilities
Maintaining optimal moisture (≤ 10-12%) and constant low temperatures to eliminate essential oil degradation and pest risks.
Fast Air Cargo & Containerized Sea Freight
Priority Air Freight
Fast airport-to-airport dispatch from Madurai & international airports to the Middle East, Europe, Southeast Asia, and North America.
- Madurai Airport priority clearance
- Insulated thermocol packaging
- 24-48 hour delivery to major hubs
- Ideal for high-grade 8mm bold cardamom
Containerized Sea Freight
FCL and LCL sea container shipments with desiccants and moisture barriers for economical bulk spice transportation.
- Full Container Load (FCL 20ft / 40ft)
- Less Than Container Load (LCL)
- Desiccant-lined moisture protection
- Direct seaport dispatch to global destinations
Export Documentation
Complete documentation package included with every shipment for seamless customs clearance at destination ports.
- Phytosanitary Certificate
- Certificate of Origin (COO)
- Commercial Invoice & Packing List
- Lab Analysis & Curcumin/Grade Certificate
5-Step Quality & Dispatch Process
Farm Procurement & Intake
Direct procurement from trusted growers followed by electronic weighing and initial sample testing.
Washing, MTRA & Destoning
Pure water washing, air winnowing, and gravity destoning remove dust, stones, and light foreign particles.
Optical Sortex & Grading
Optical color sorting isolates discolored seeds, separating spices into 7mm, 8mm, and bold export grades.
Clean Room Hygienic Packing
Airtight vacuum foil packing, thermocol-lined cartons, and multi-wall food-grade bags preserve natural spice aromas.
Container Stuffing & Export Dispatch
Factory container stuffing with moisture absorbents, phytosanitary clearance, and rapid dispatch to sea/air cargo hubs.
Elevate Your Fragrance & Ingredient Supply Chain with Premium Natural Extracts
Partner with SPD Exports for high-quality floral extracts, essential oils, and natural essences crafted for the global perfume, fragrance, cosmetic, and wellness industries. We provide carefully sourced botanical ingredients with consistent quality, customized solutions, and reliable worldwide export support.